Product Research & Development is a core phase dedicated to driving innovation and refining new solutions.
The key stages of this process include:
- Data Mining
- Development
- Sample Preparation
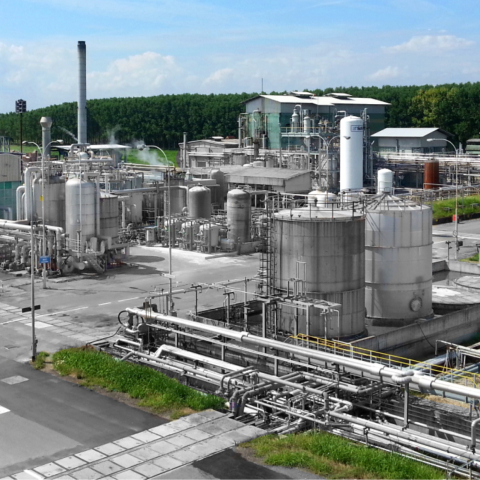
Our Contract Manufacturing division is a cornerstone of Sipcam Oxon’s global operations. It’s more than just a network of plants, it’s a coordinated system where each site brings unique strengths to the table, providing integrated toll manufacturing services and custom chemical manufacturing capabilities through an international network of specialized plants.
Depending on the location, we handle the synthesis of active ingredients and chemical intermediates, as well as custom formulation, toll blending, packaging and logistics for crop protection products, special fertilizers, biostimulants and seed treatment solution.
High-precision solid microgranule impregnation engineered for targeted, uniform field application with zero dust generation.
Where we are
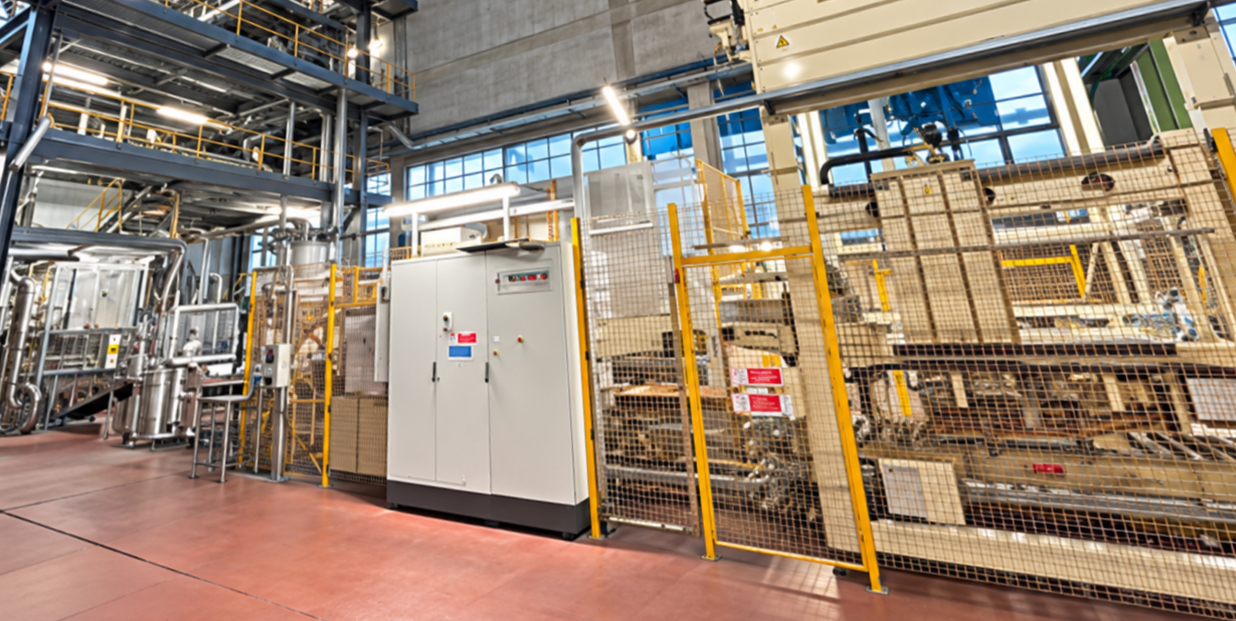
Micronized wettable powder formulations delivering superior wettability and suspensibility, optimized for maximum tank-mix stability.
Where we are
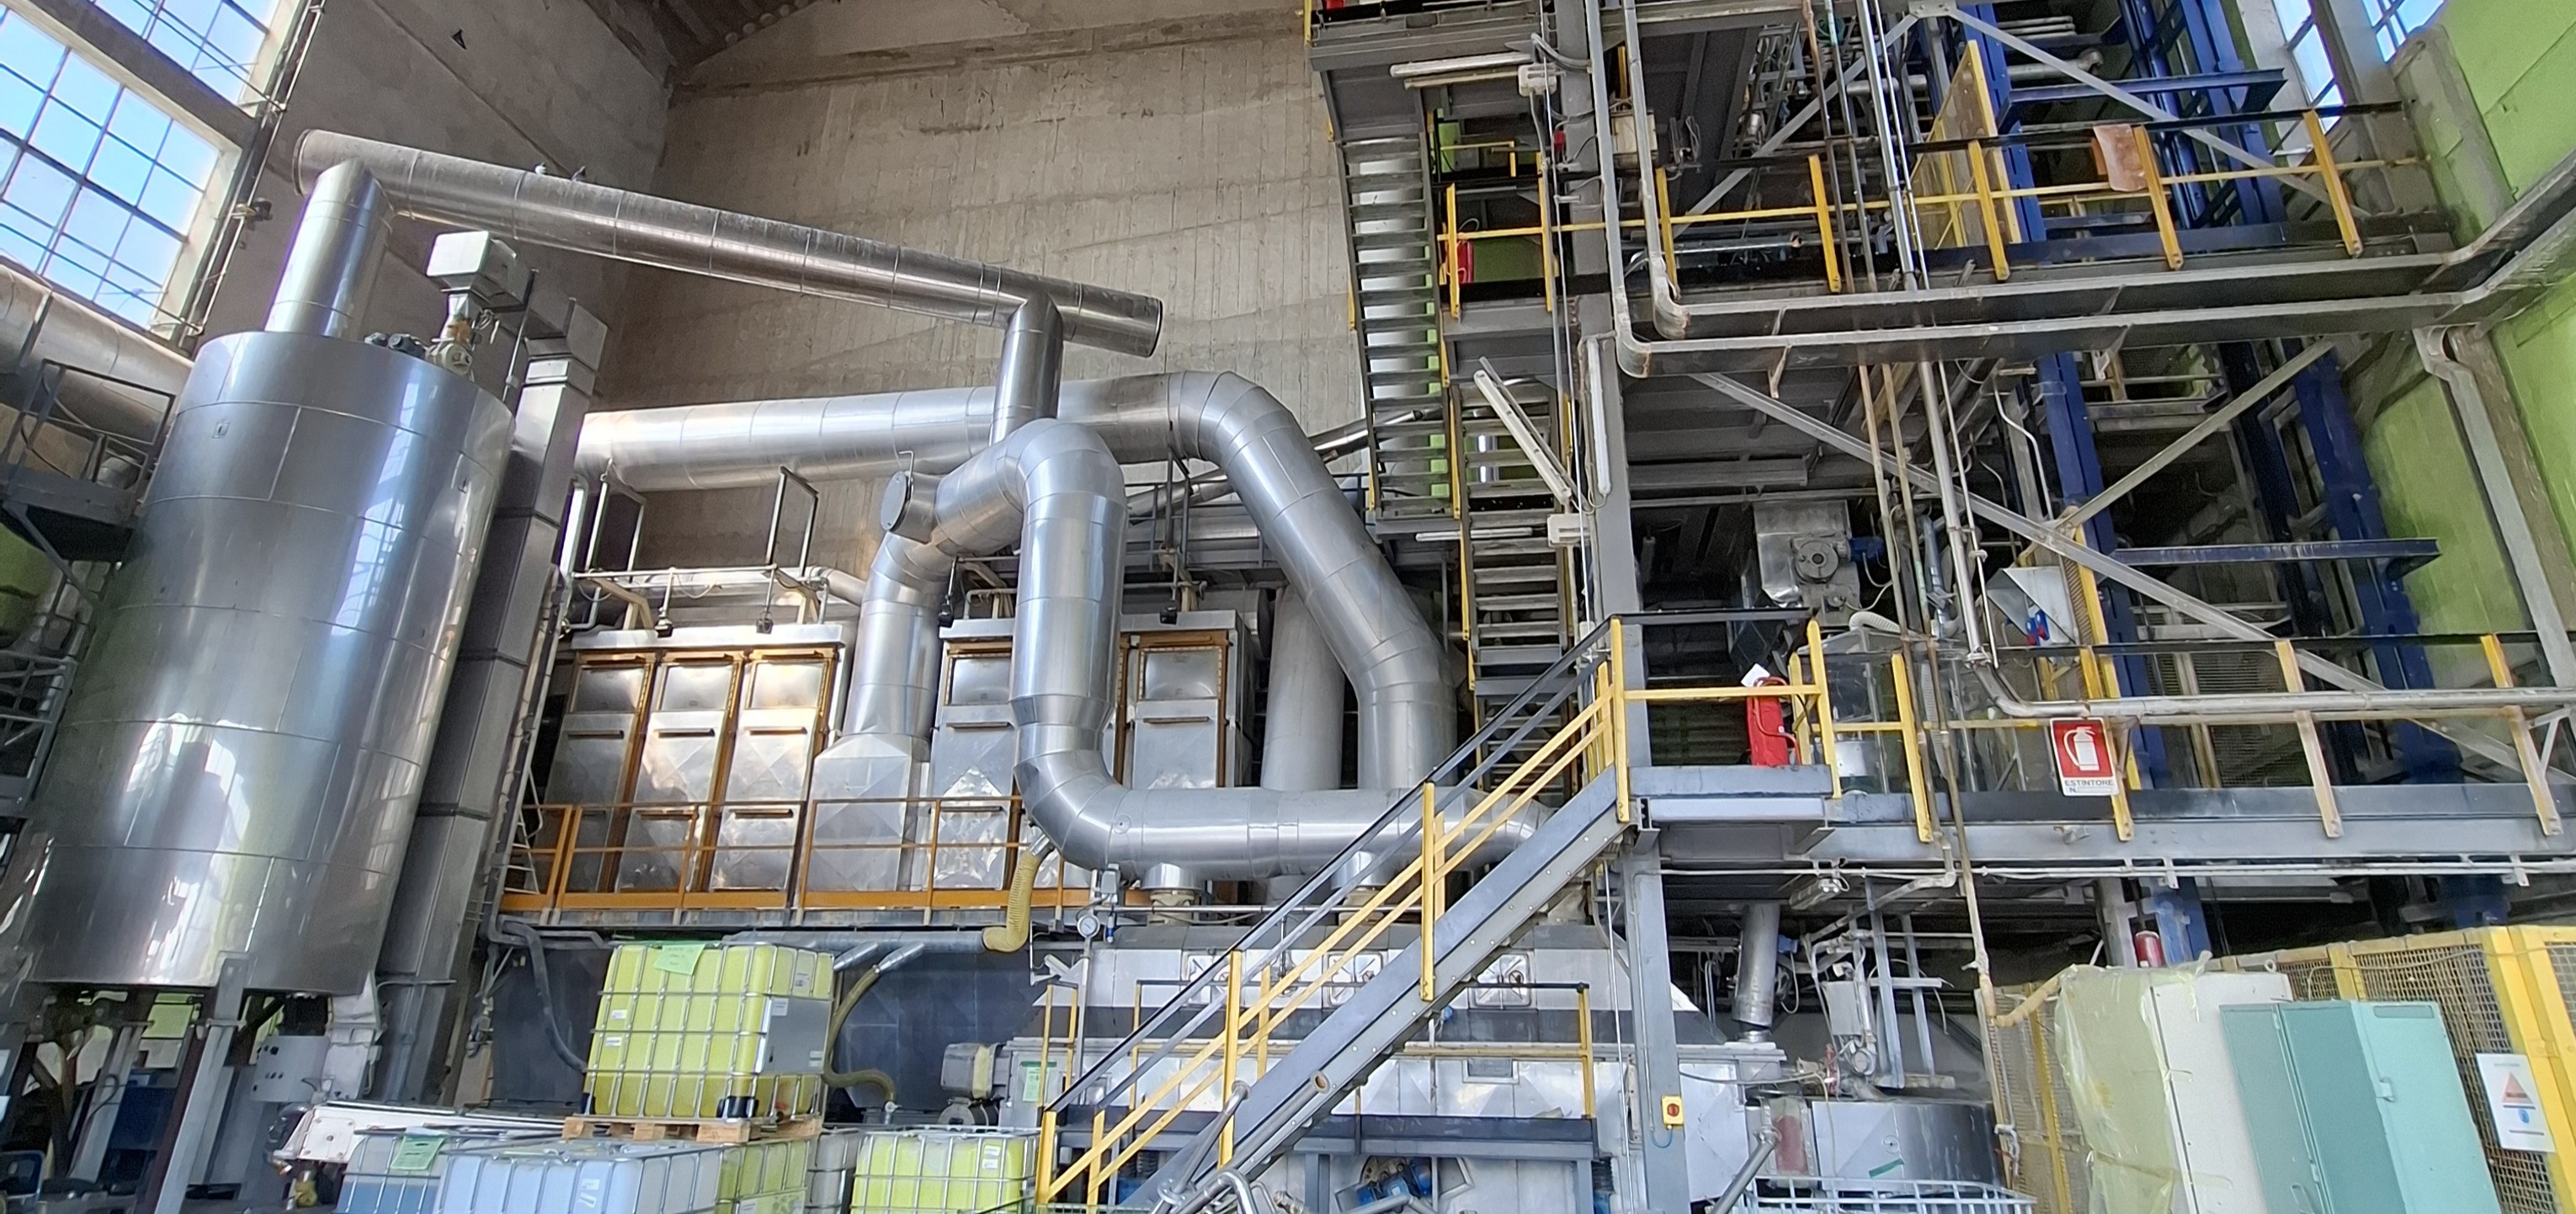
Advanced water-based flowables developed through specialized wet-milling to ensure exceptional long-term physical stability and dispersion.
Where we are
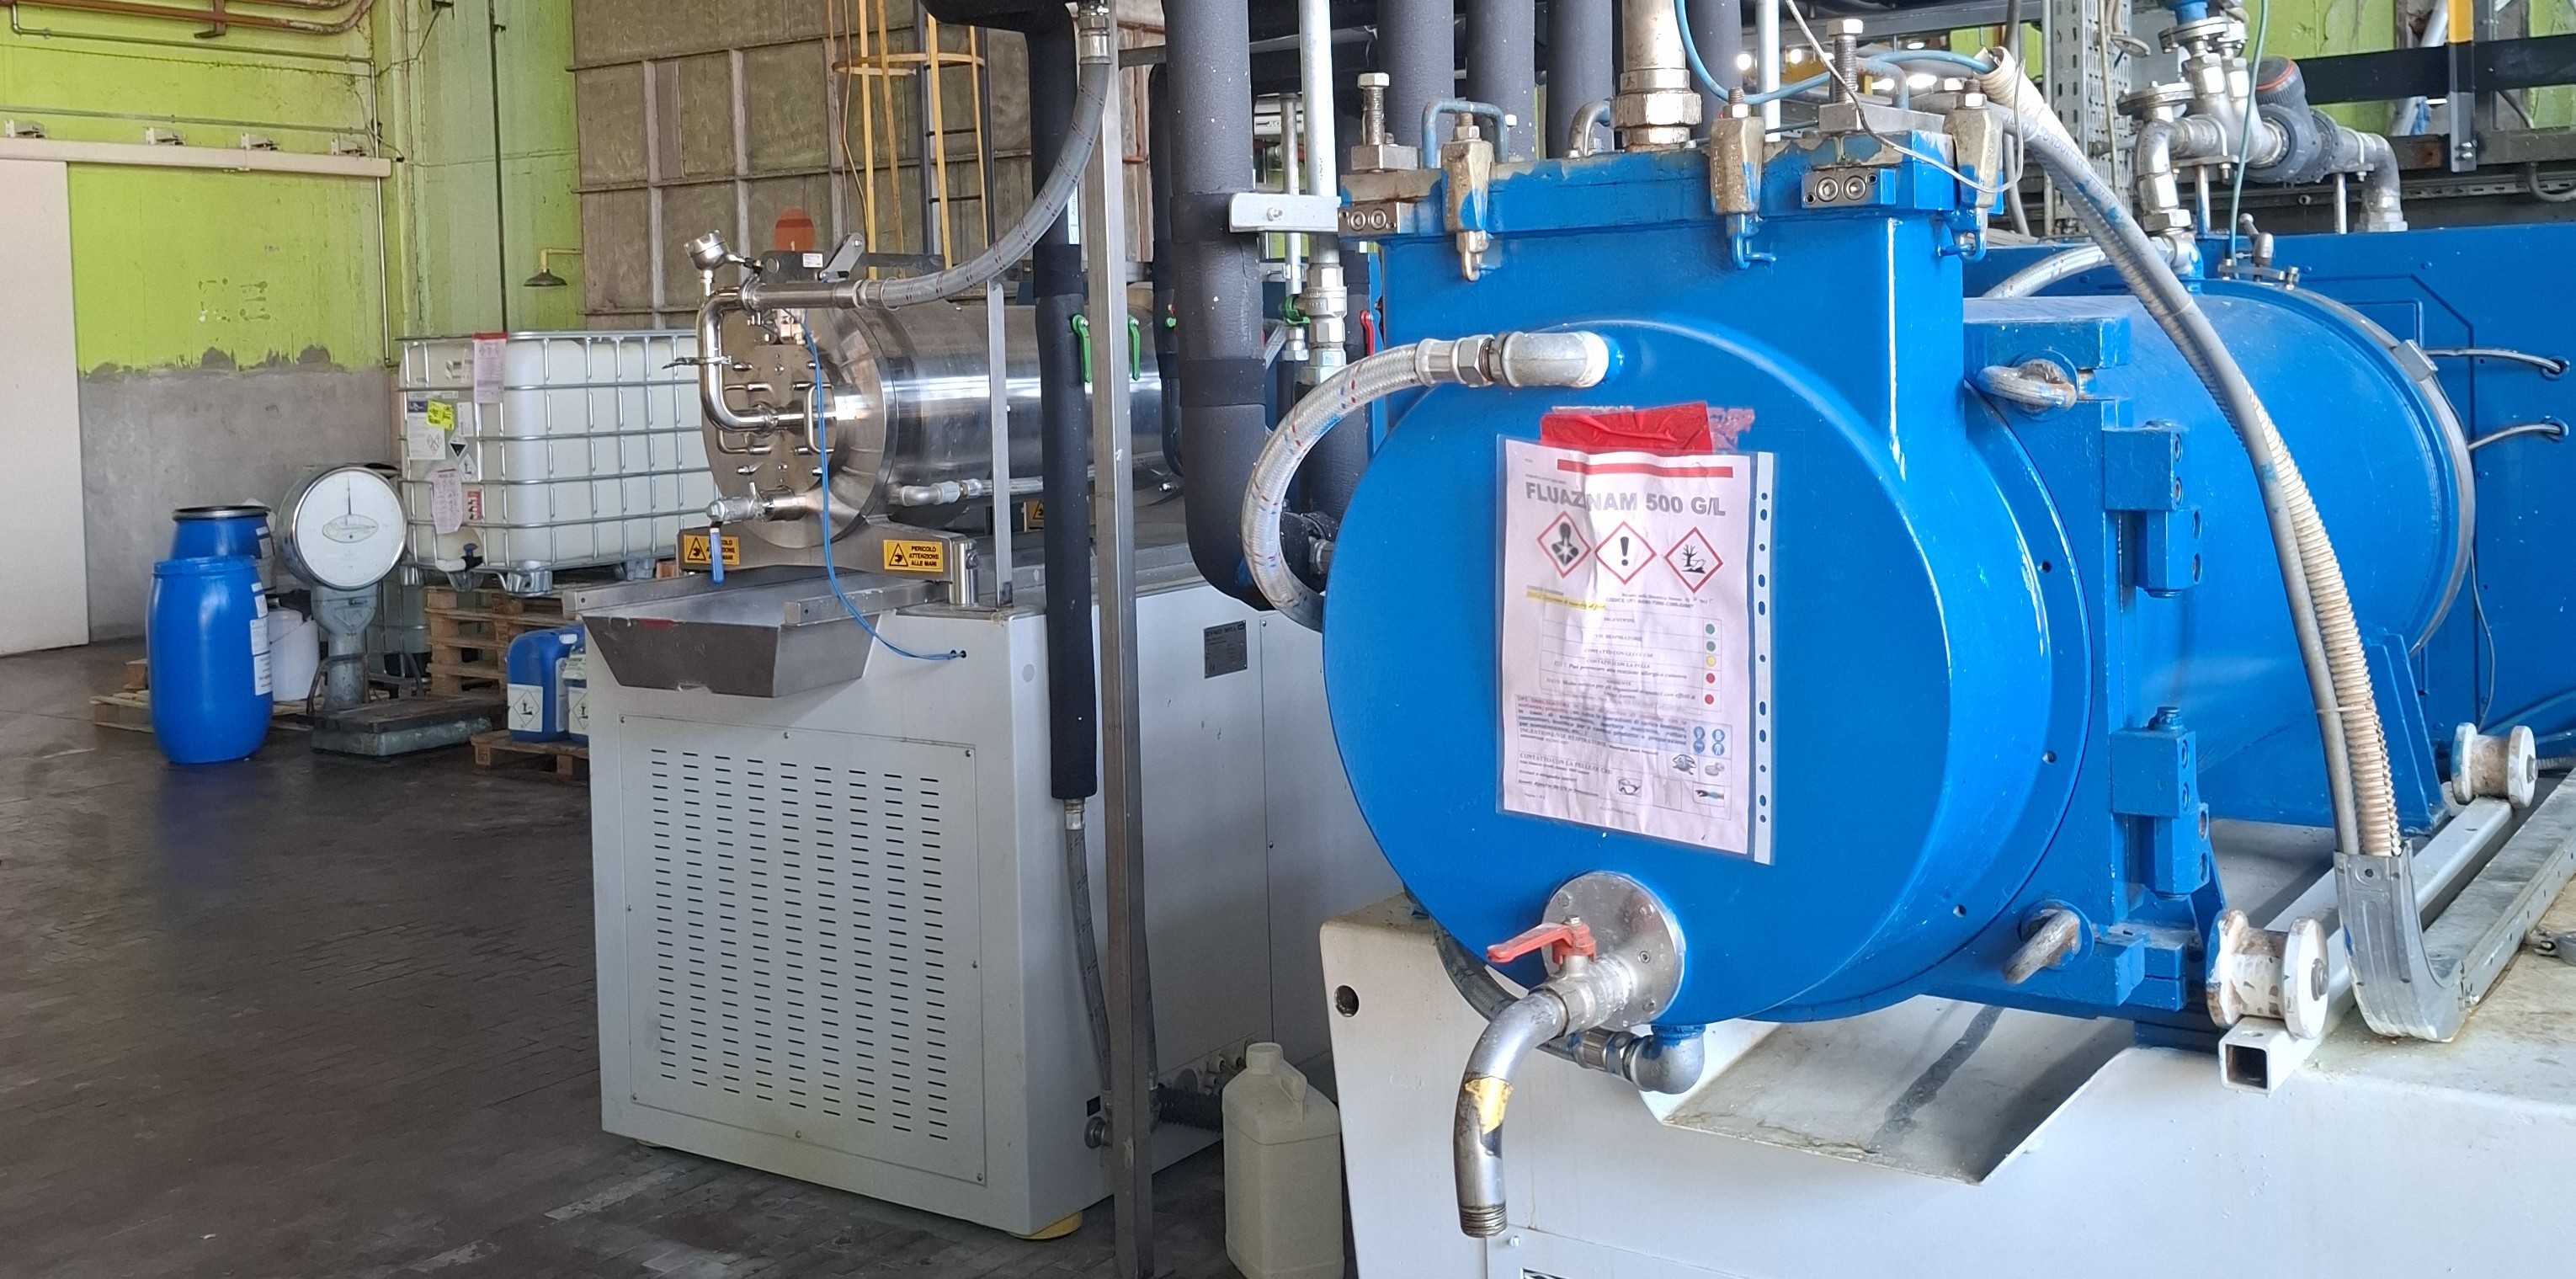
Cutting-edge microencapsulation technology designed for controlled active ingredient release, maximizing efficacy and operator safety.
Where we are
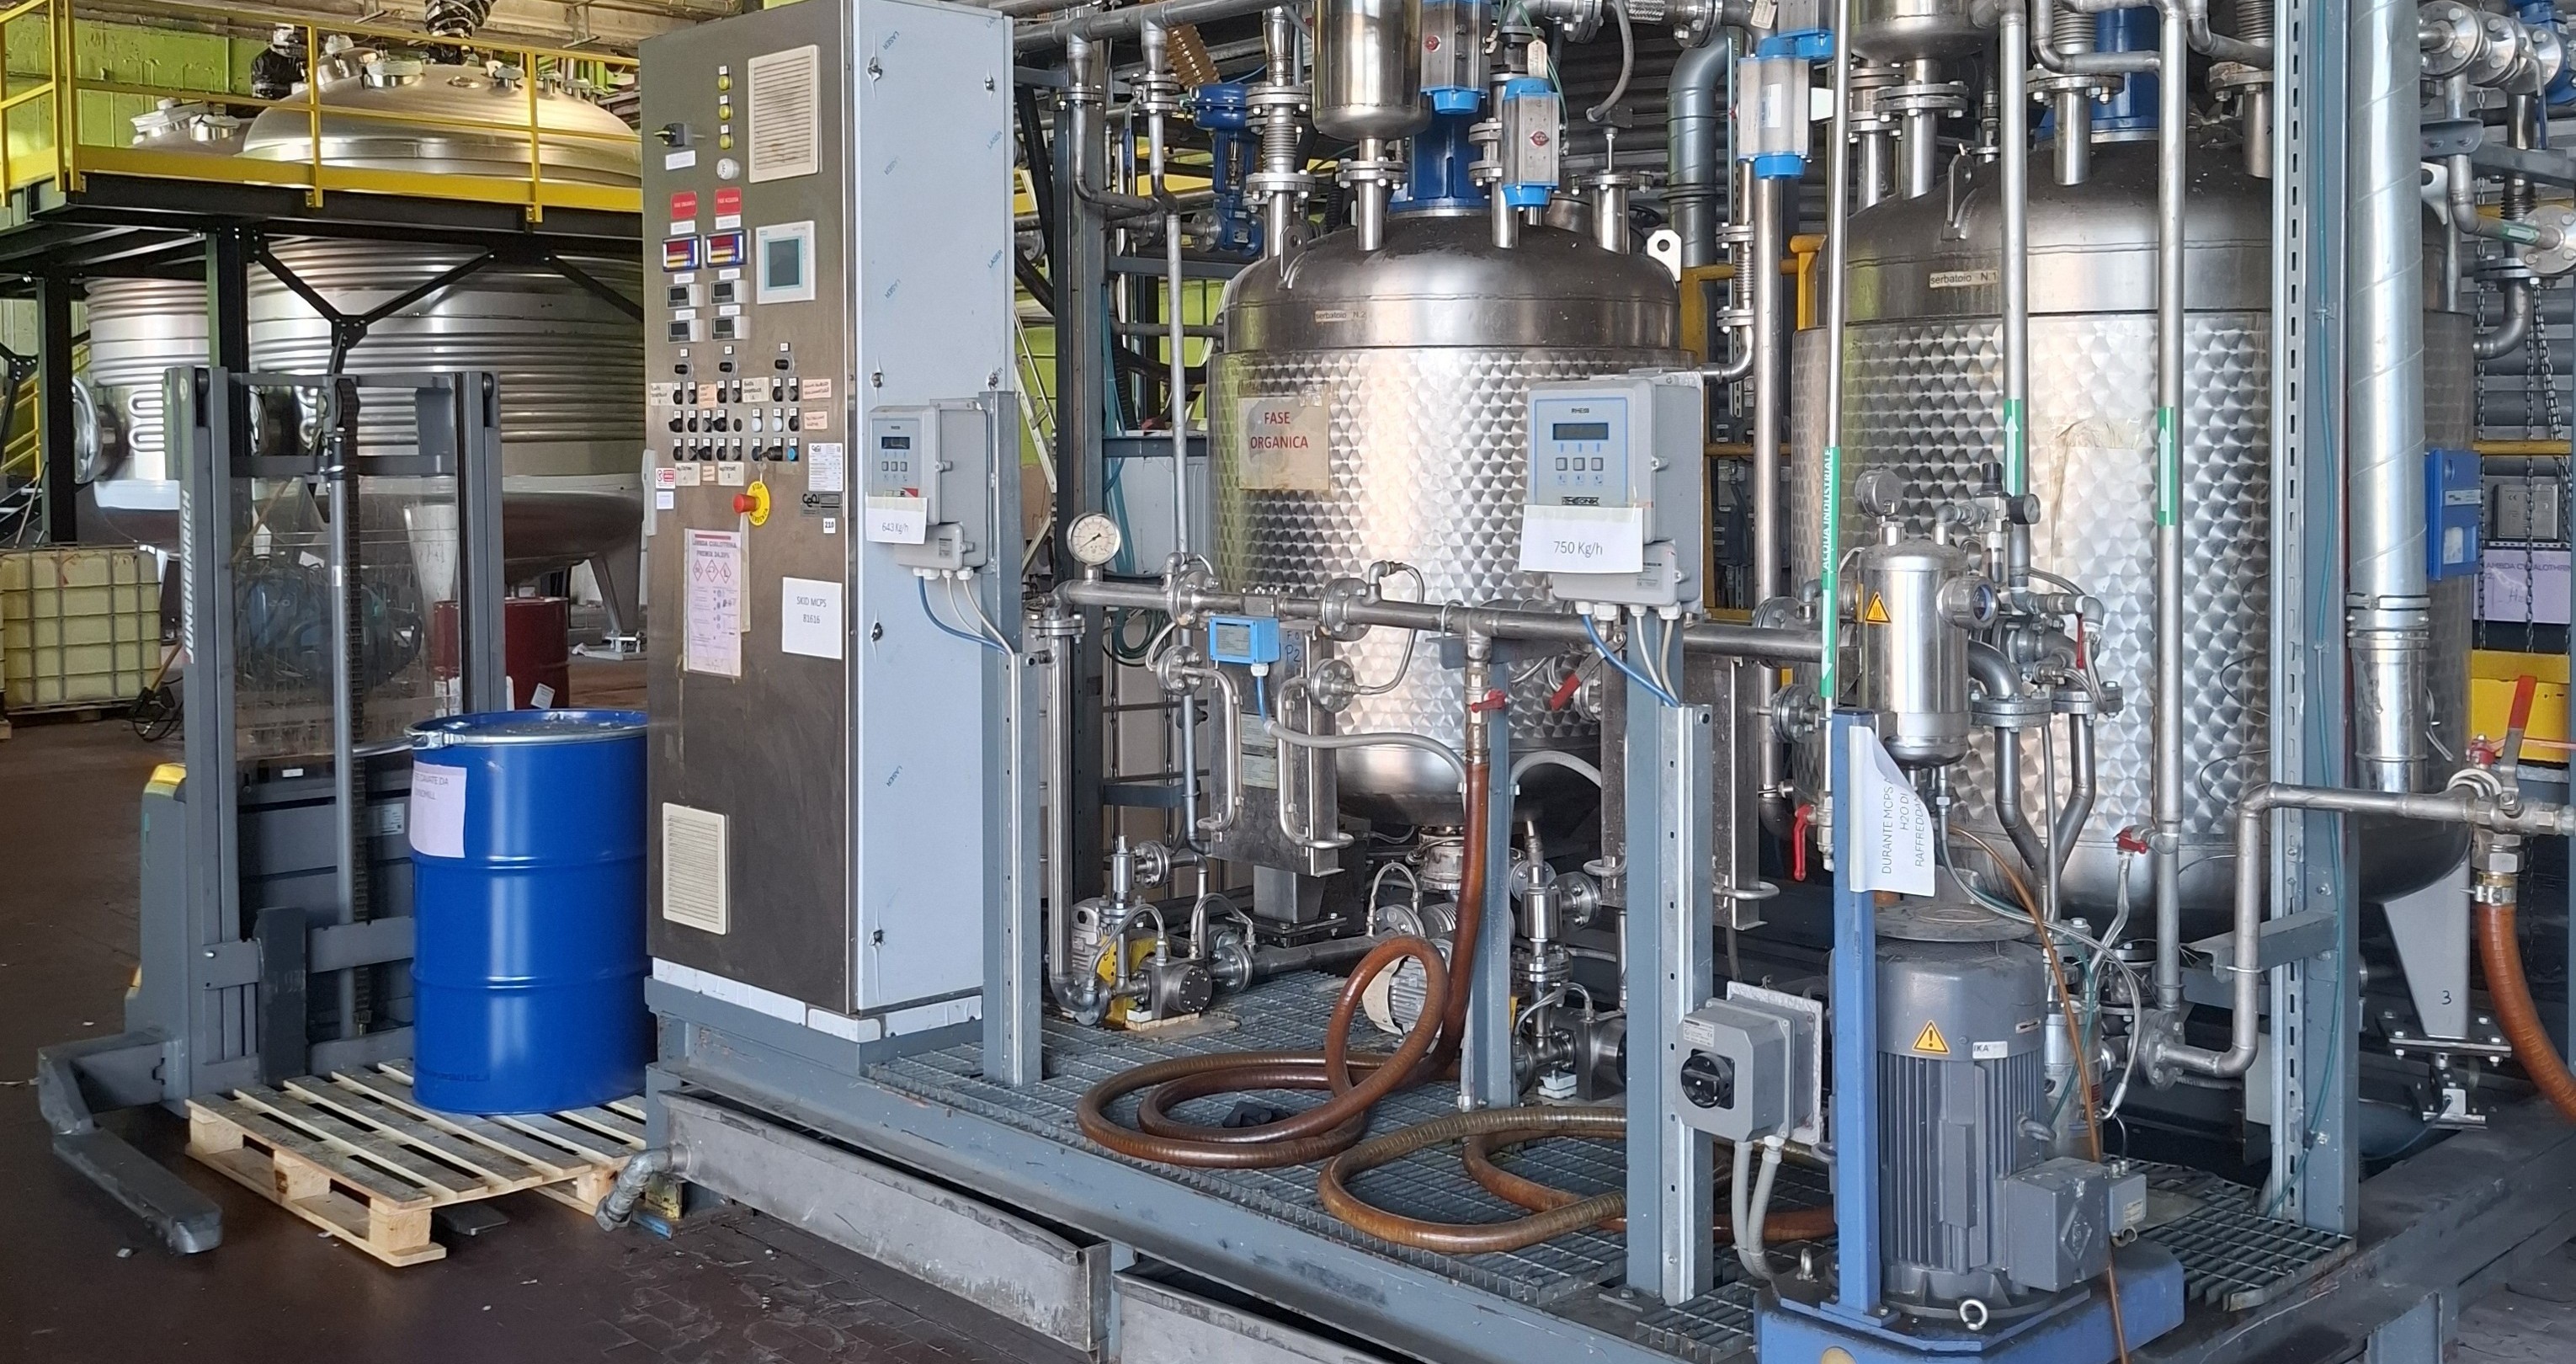
Complex liquid systems - from emulsifiable concentrates to microemulsions - engineered for optimal active delivery and superior thermal stability.
Where we are
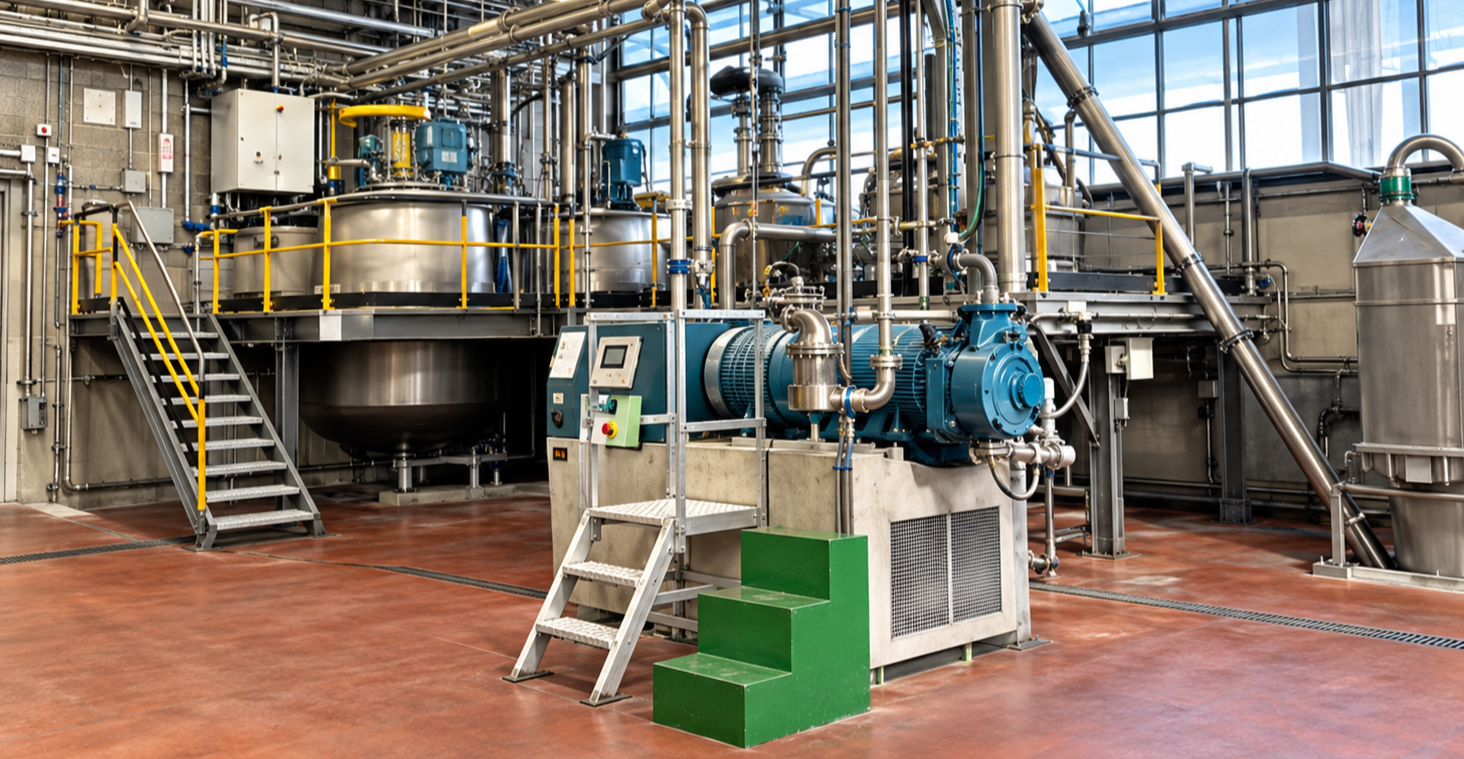
Top-tier dry flowable and soluble granulation, combining dust-free handling and precise dosing with rapid, complete dissolution.
Where we are
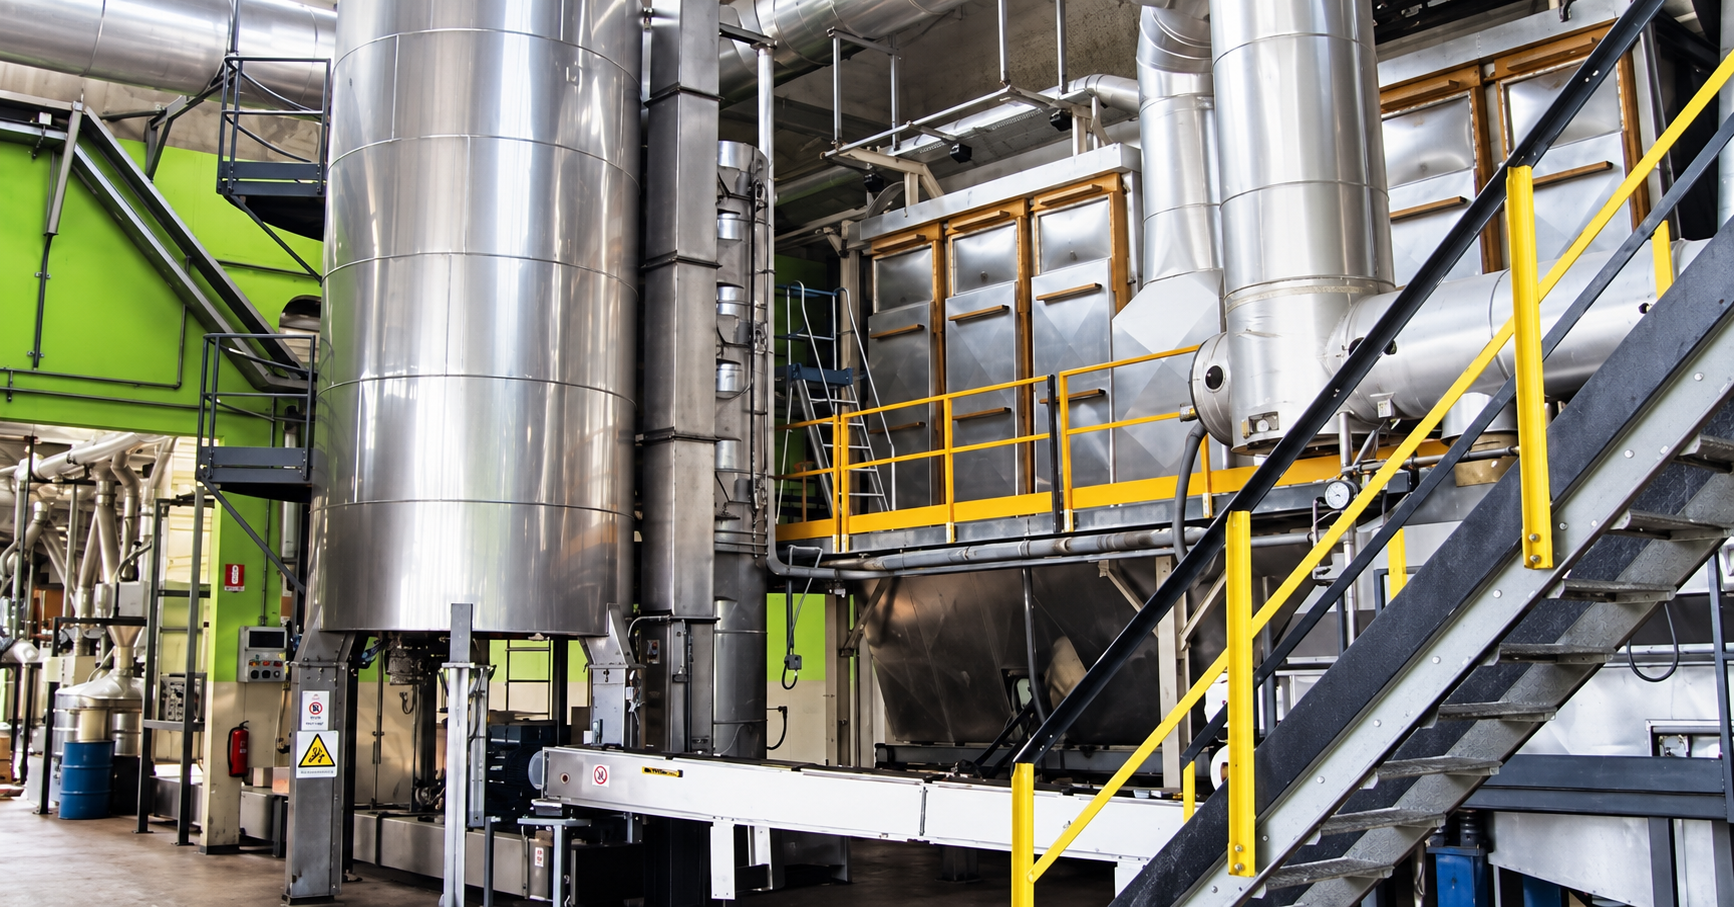
Advanced thermal-controlled liquid formulations, utilizing precise heating and cooling reactions to preserve amino acid integrity and optimize micronutrient complexation for superior crop resilience.
Where we are
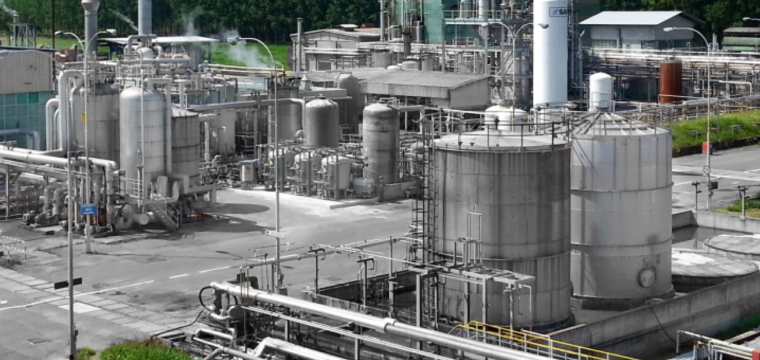
The main manufacturing formulation plant with a surface area of 300,000 m². This site, which produces about 25,000 tons of formulated products per year, is one of the most technologically advanced in the world. In addition to classic formulations, the site produces more innovative formulations, such as microencapsulated and water-dispersible granules.
Formulations
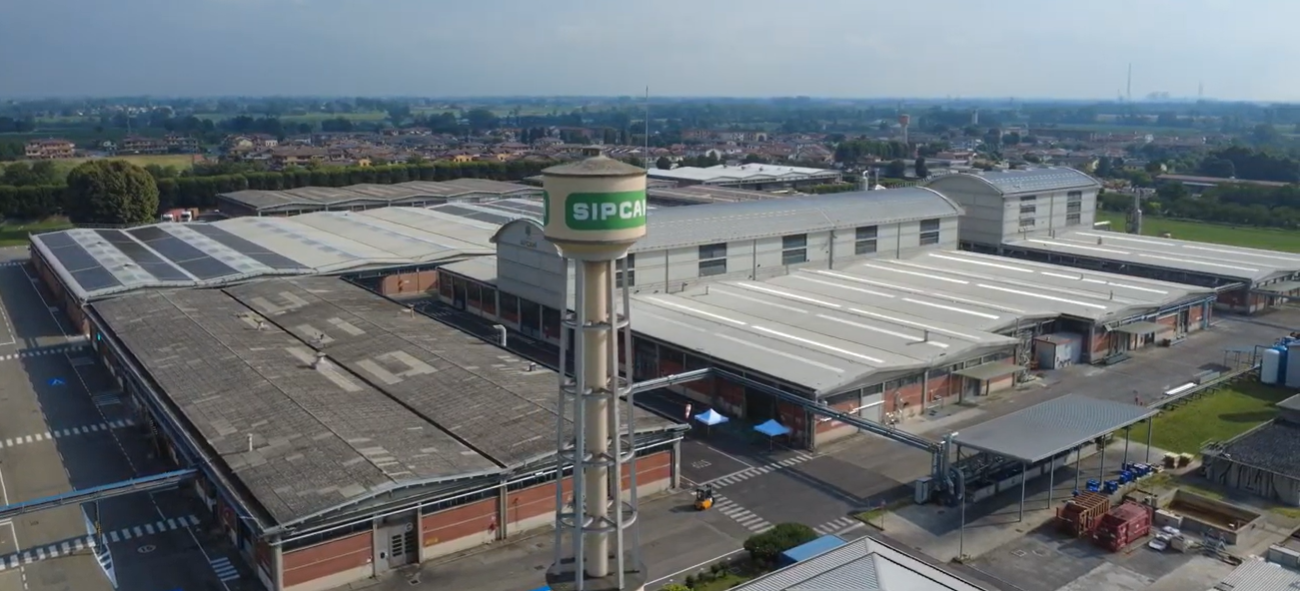
The plant has separated areas to formulate special fertilisers, biostimulants and crop protection products. With a total surface area of 92,000 m², it annually produces around 12,000 tons of plant protection products and 9,000 tons of biostimulants and special fertilisers, with vast expertise in developing and formulating high quality and innovative products.
Formulations
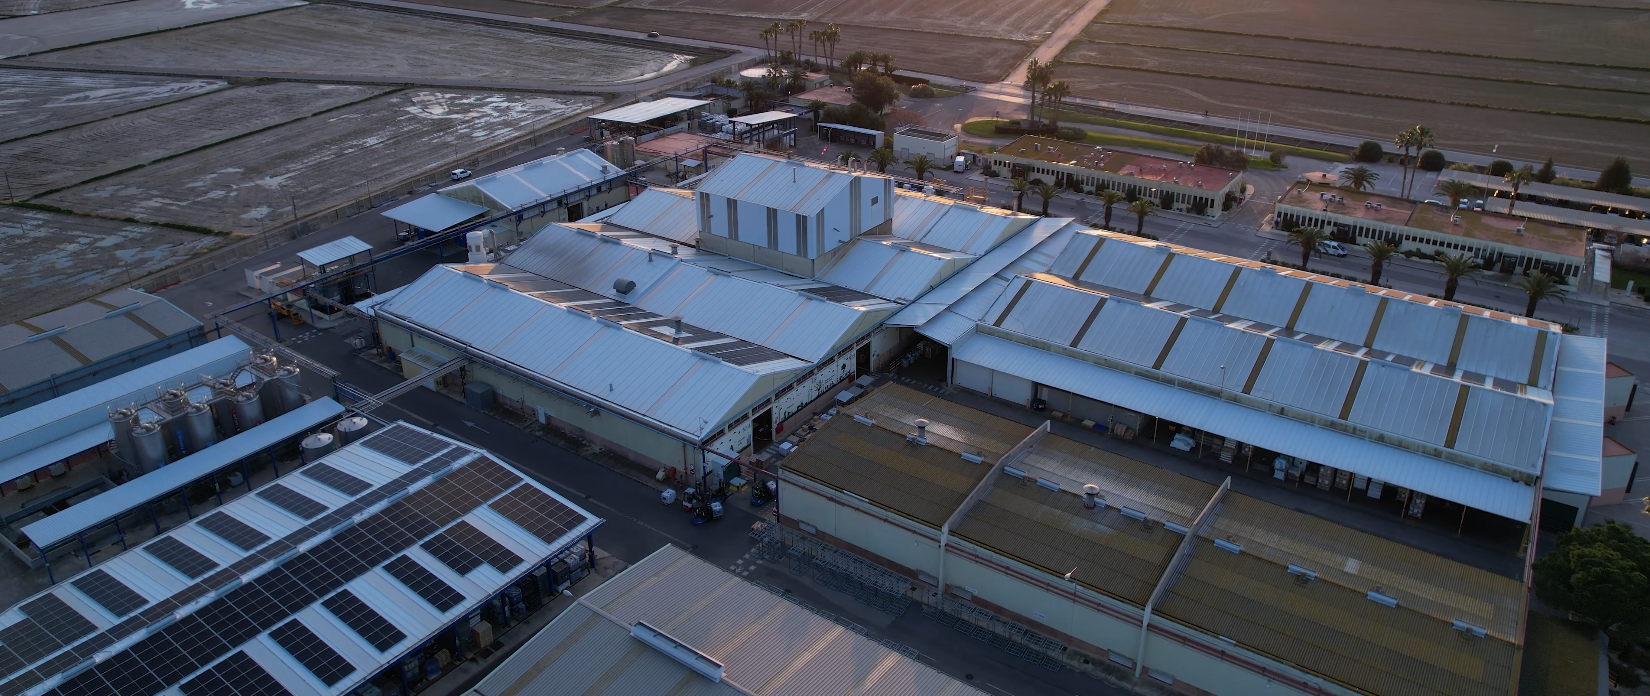
Formulation, packaging, tolling, and logistics of Fungicides, insecticides, and herbicides for agriculture
Formulations
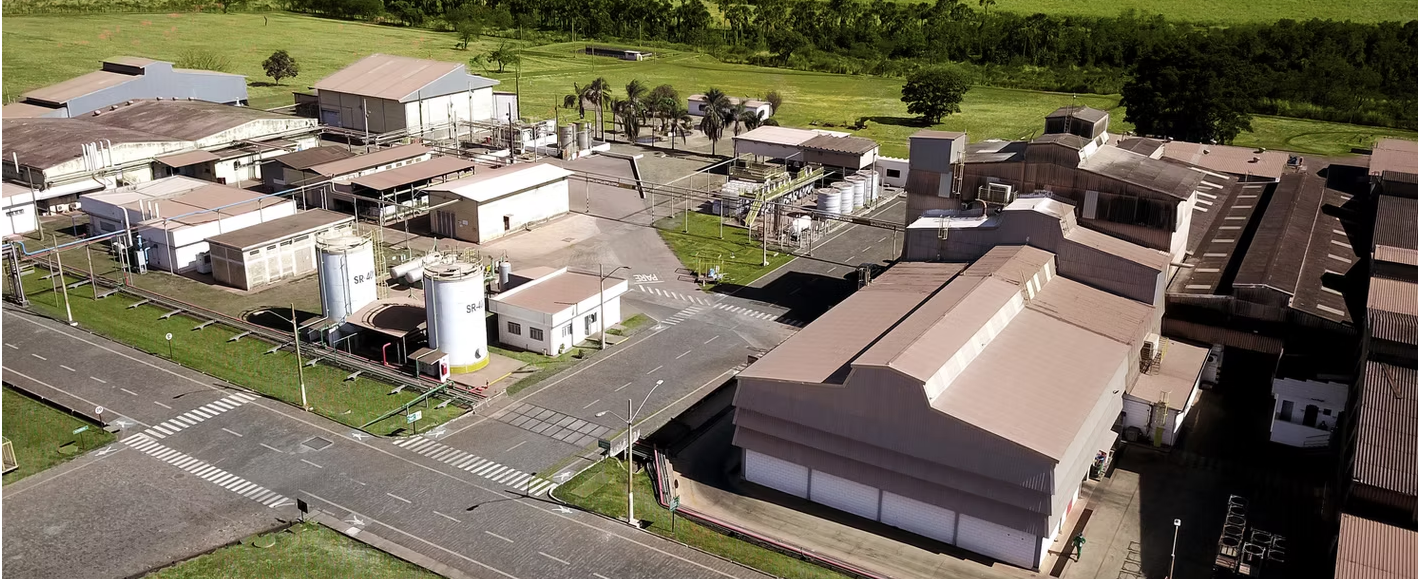
Formulation and third-party production plant
Formulations
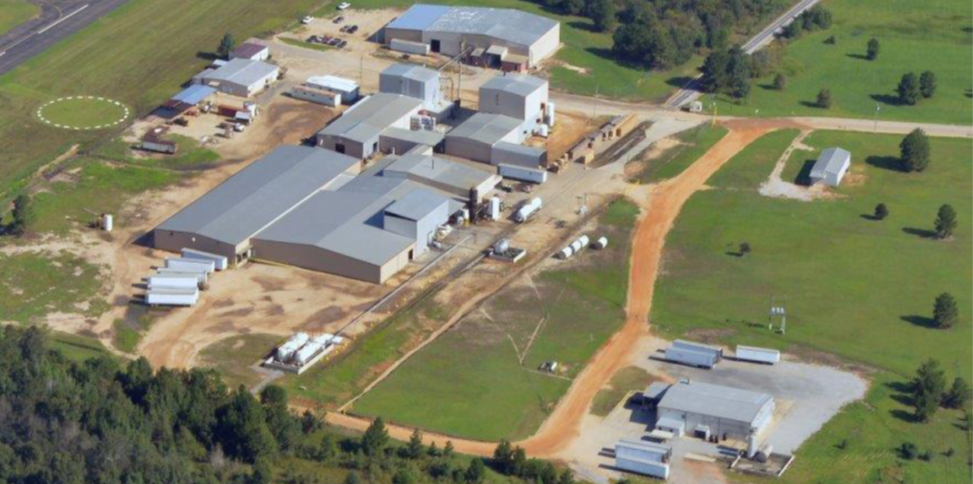
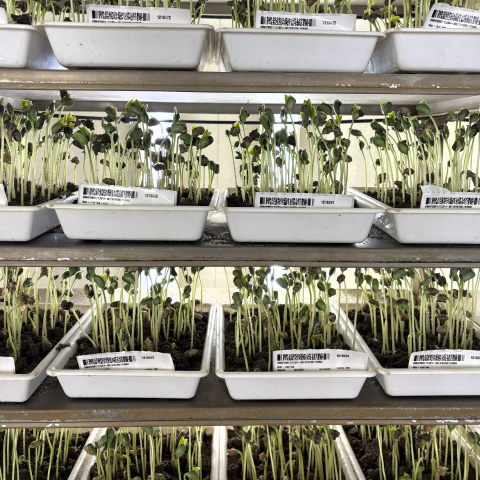
The Lodi plant has a total site surface area of 20,000 m² and is dedicated to seed treatment, laboratory analysis, packaging and storage. It processes up to 8,500 tons of soybean seed and 2,000 tons of corn seed per year.
Seed processing
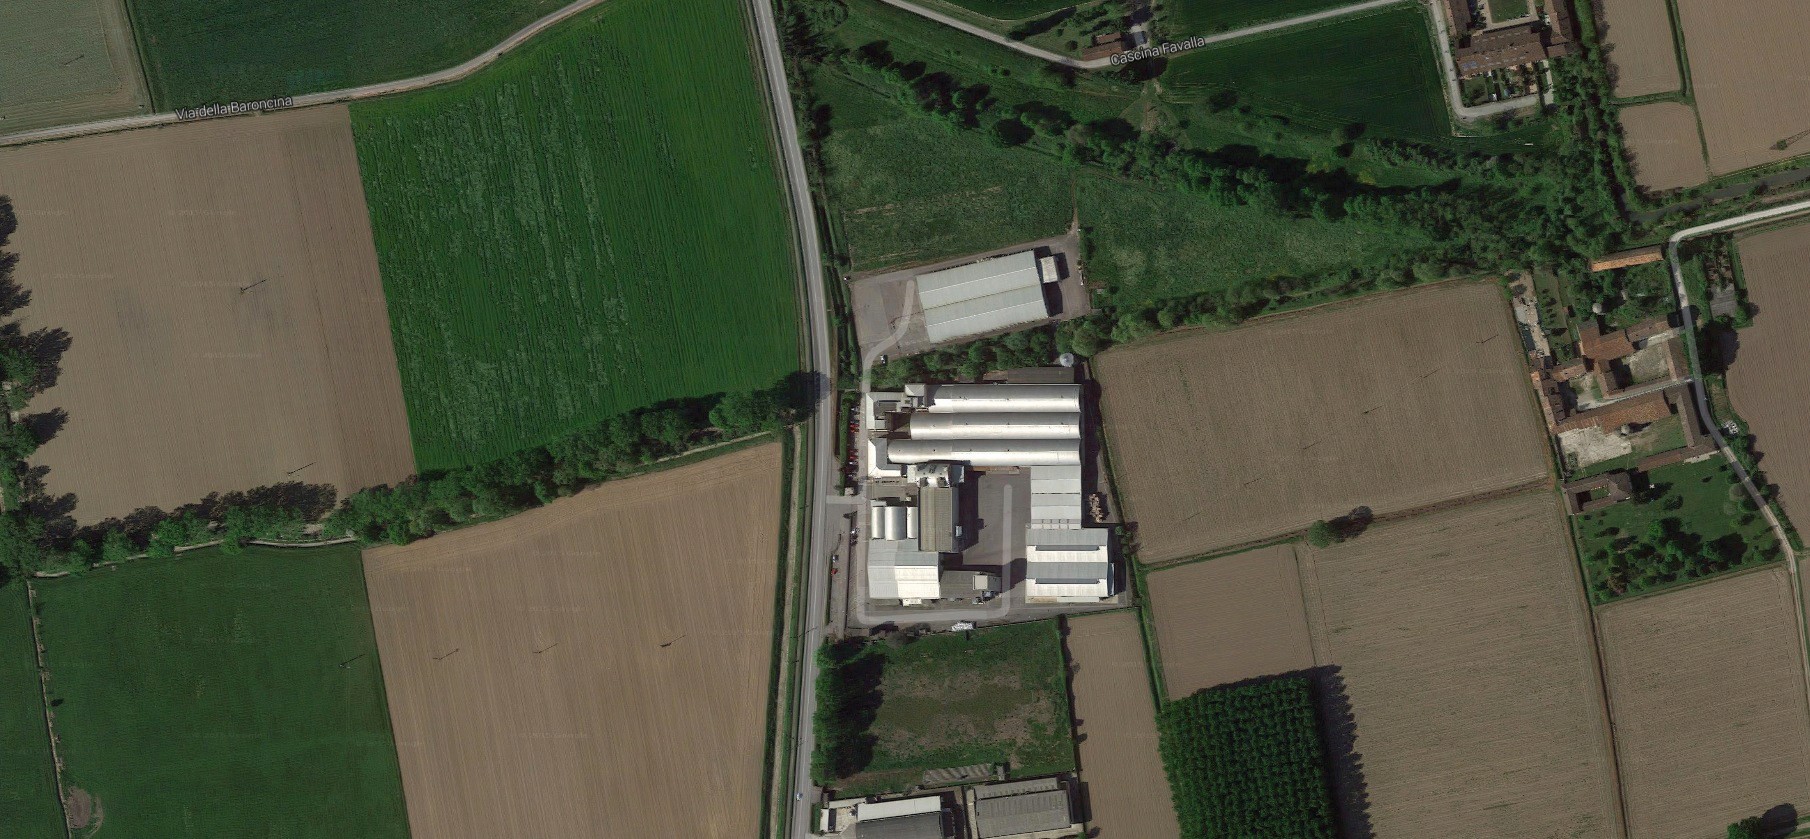
The manufacturing formulation plant with a total site surface area of 5,000 m² (including a 2,000 m² warehouse). This site, which produces about 3,000 tons of formulated products per year, is highly specialized in agricultural solutions. The site focuses on liquid formulations involving plant nutrients and biostimulants, managing advanced processes from heating and cooling reactions to bulk solubilising, blending, packaging and logistics.
Liquid formulations
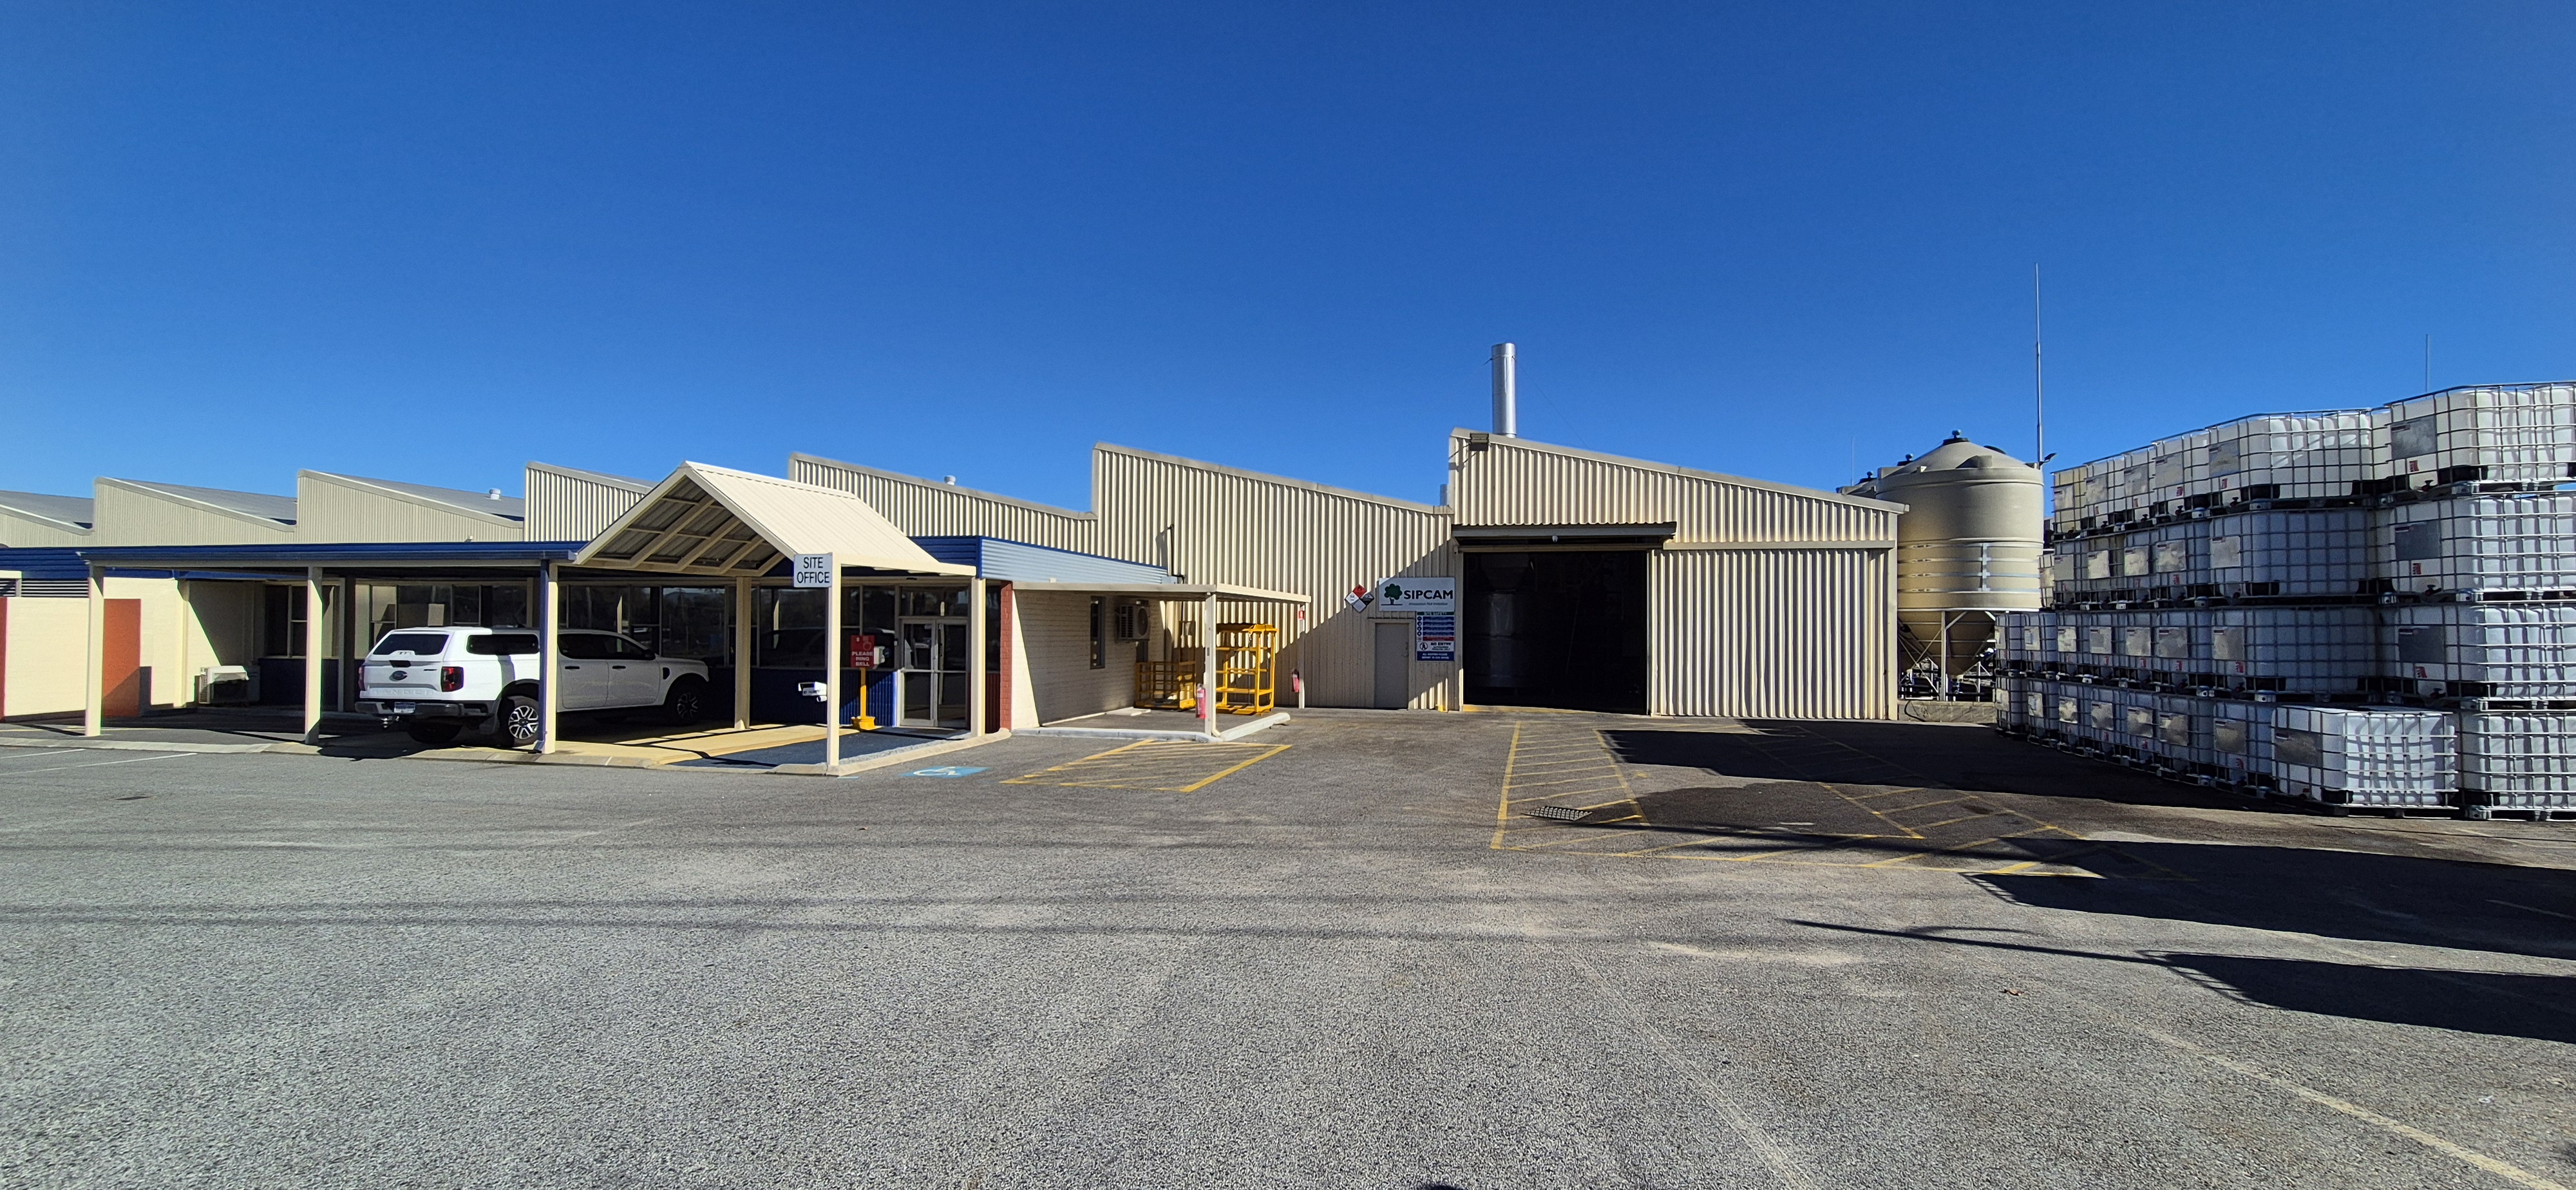
The manufacturing formulation plant with a total site surface area of 8,000 m² (including a 3,000 m² warehouse). This site, which produces about 8,000 tons of formulated products per year, is highly specialized in agricultural solutions. The site focuses on liquid formulations involving plant nutrients and biostimulants, managing advanced processes from heating and cooling reactions to bulk solubilising, blending, packaging and logistics.
Liquid formulations
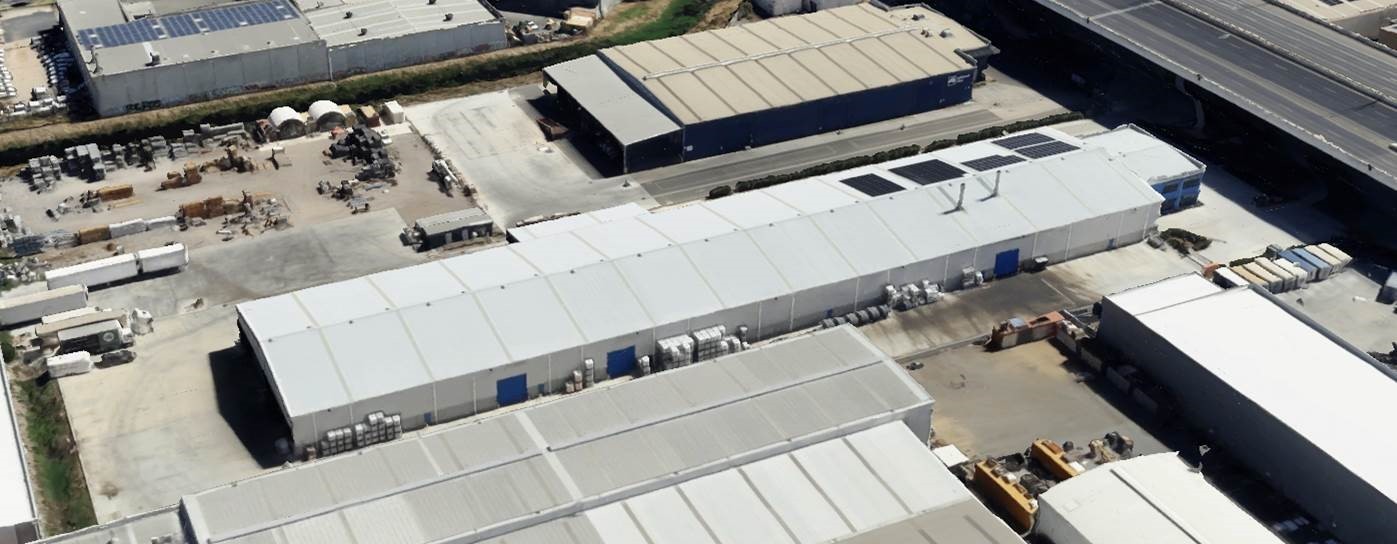
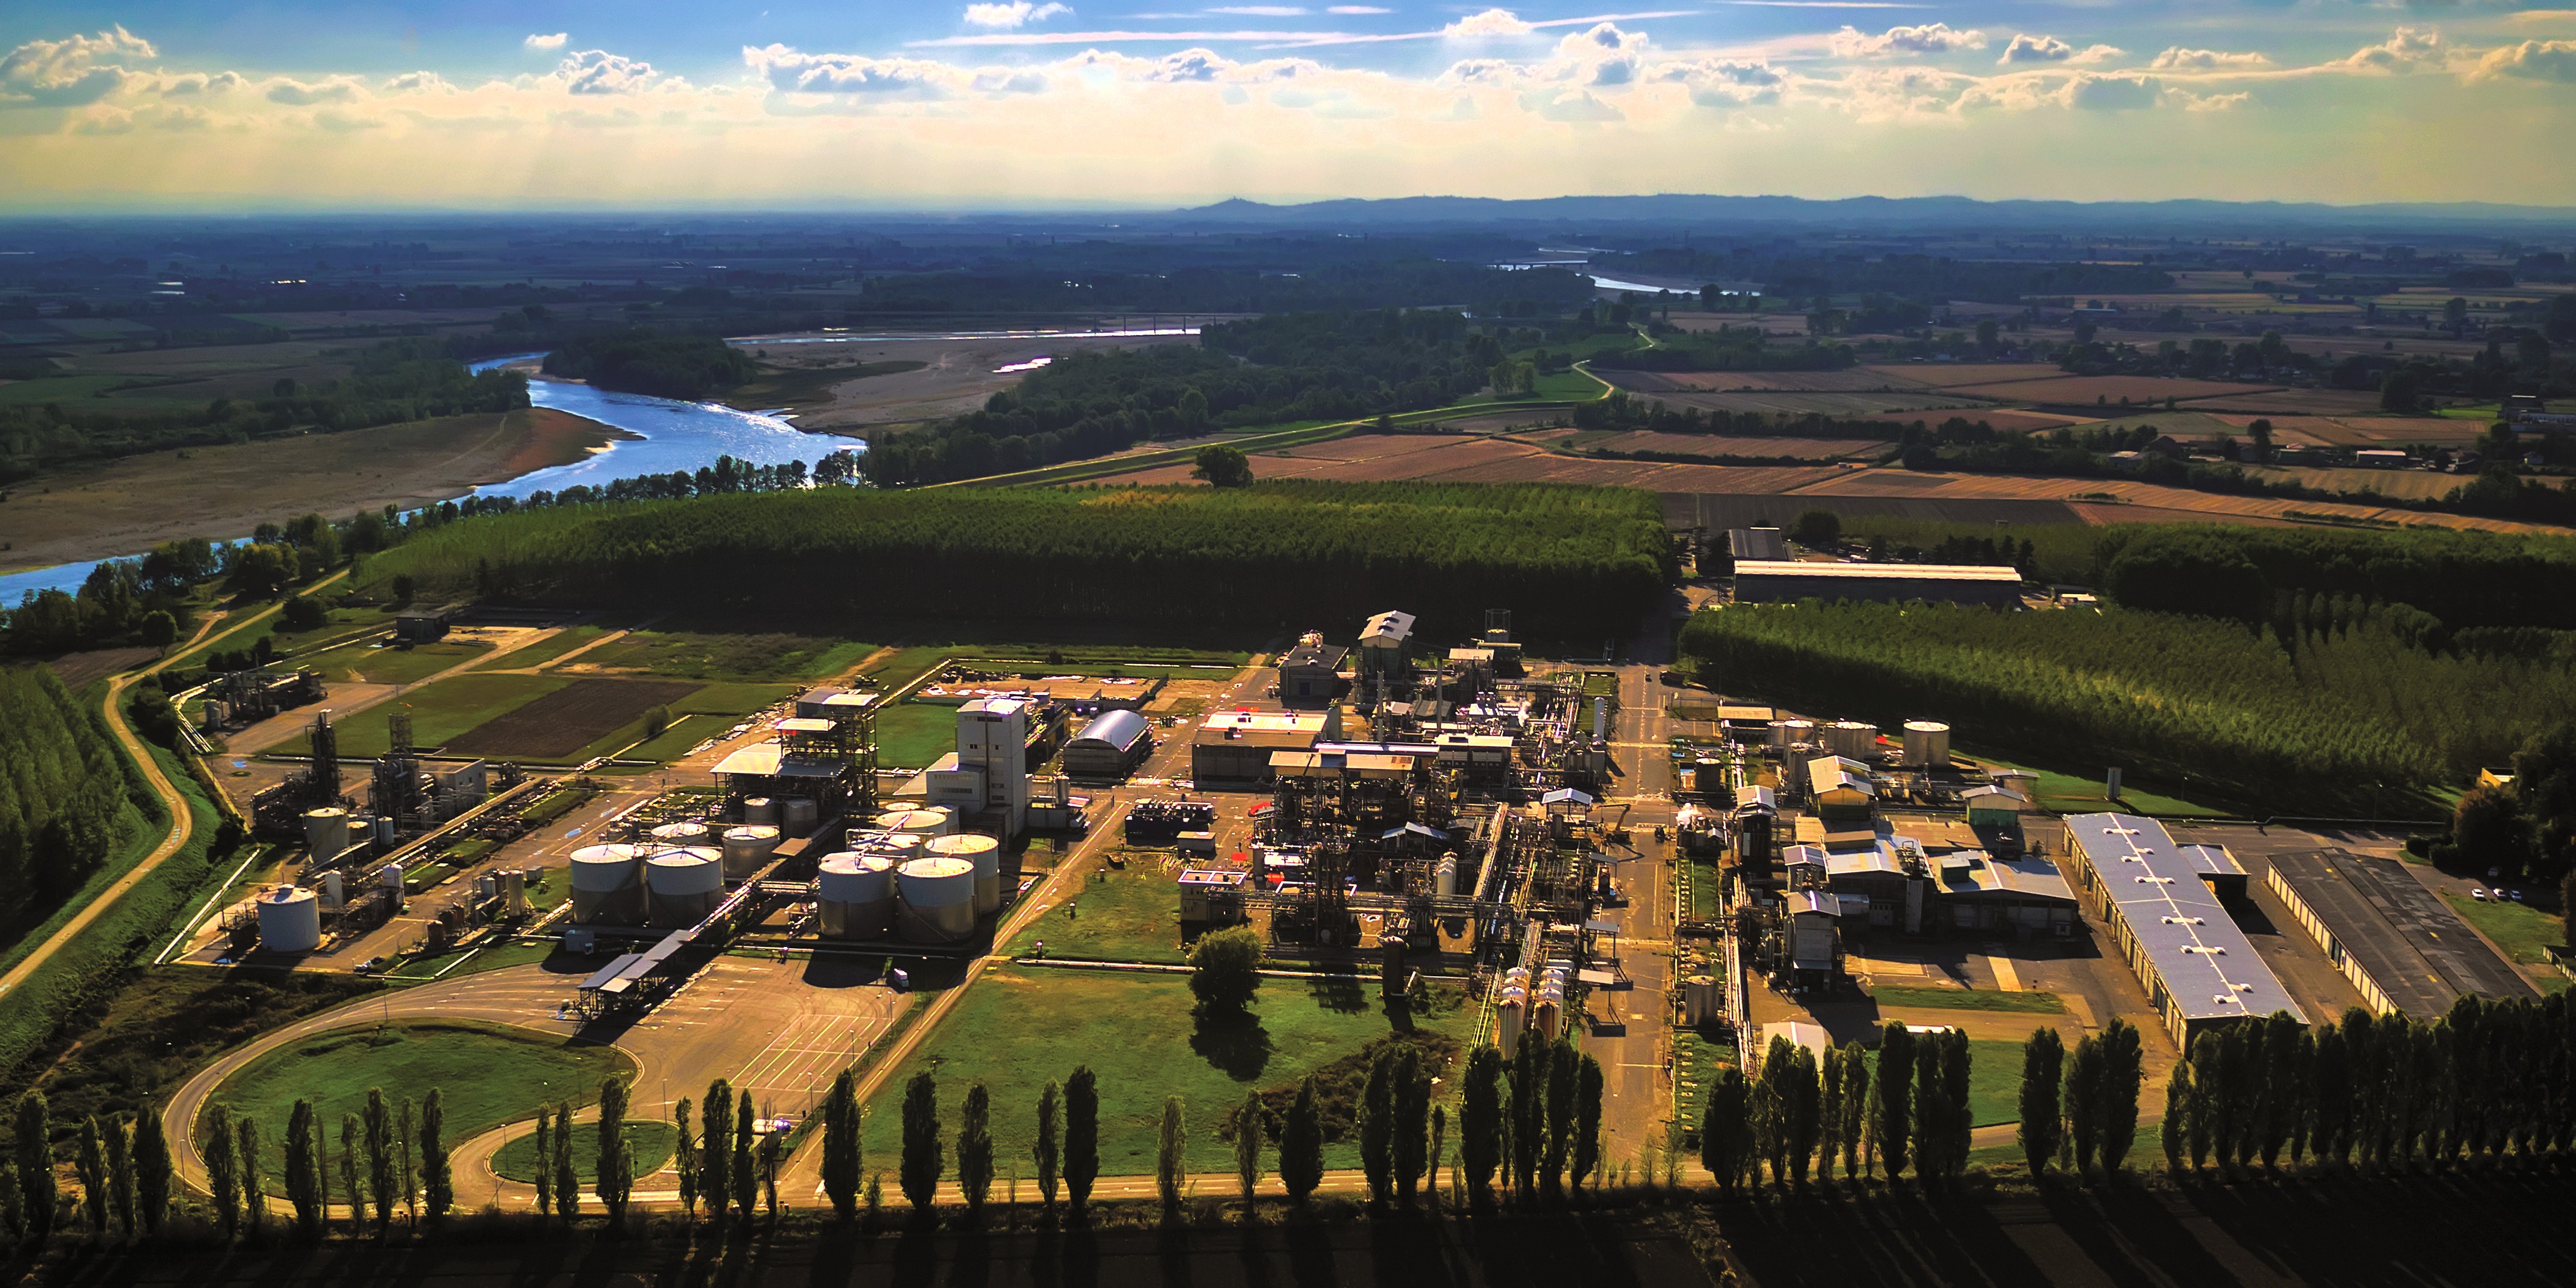
A covered area of 600,000 m² of which 100,000 m² is industrialized. The plant synthesises around 20,000 tons per year of active ingredients and was the first in Italy to obtain UNI 10617 (Safety Management Systems) certification, to which ISO 9001 was added. A plant for the synthesis of clomazone was built, in addition to the one for triazine family herbicides and chemical intermediates production. Two electricity production plants power the site, one traditionally powered and the other powered by renewable sources.
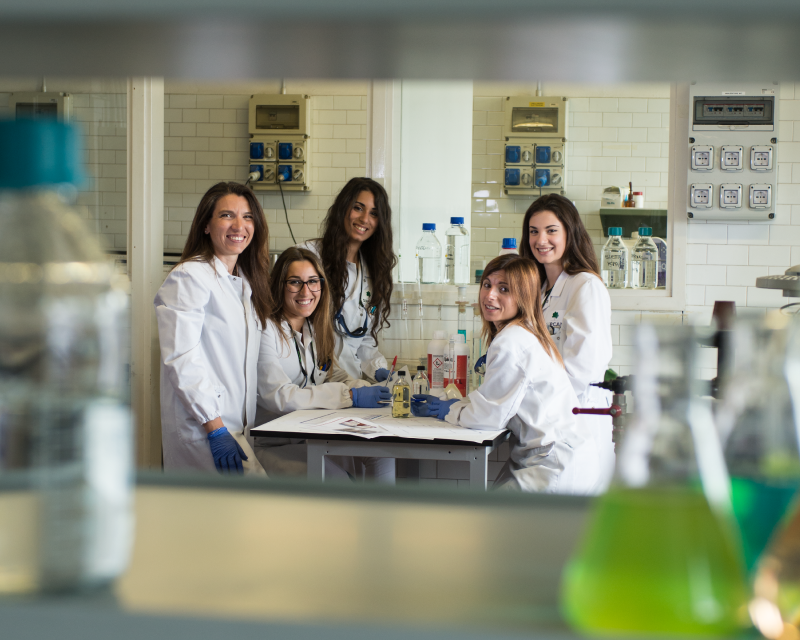
Product Research & Development is a core phase dedicated to driving innovation and refining new solutions.
The key stages of this process include:
Our capabilities cover chemical synthesis of active ingredients as well as intermediates, customizing our chemical to offer the best solutions to our clients.
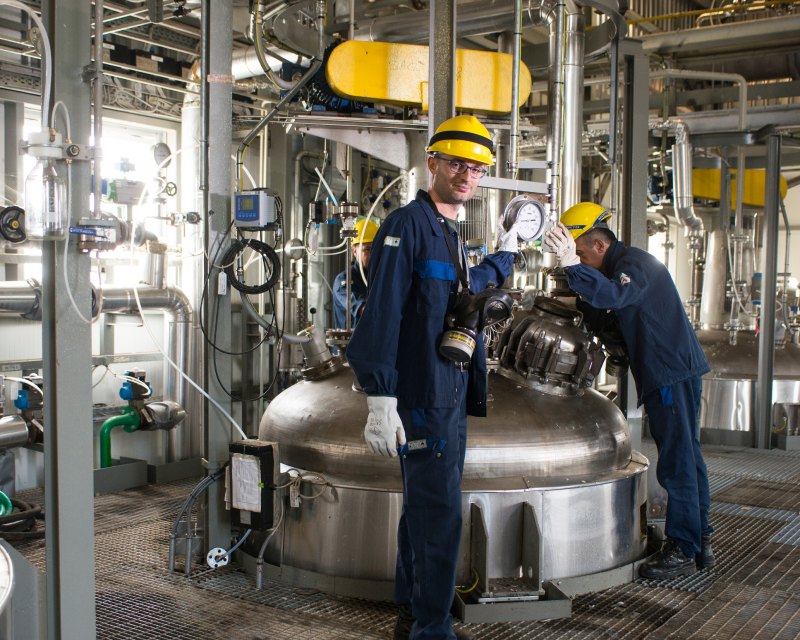
We manufacture high quality products by using the most advanced and proprietary technologies. We offer most of the technology solutions to meet our client requirement.
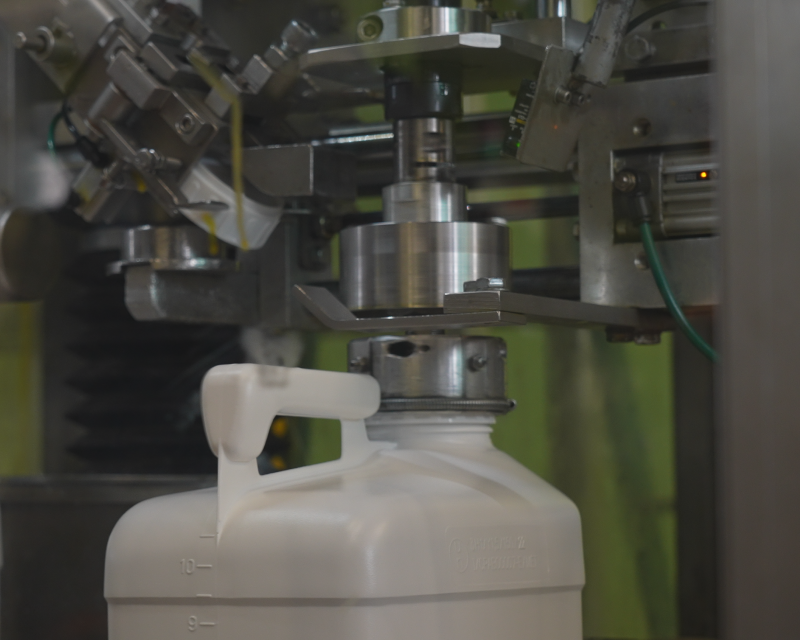
We take care of packaging of both liquid and sold forms, preparing the product for distribution worldwide.
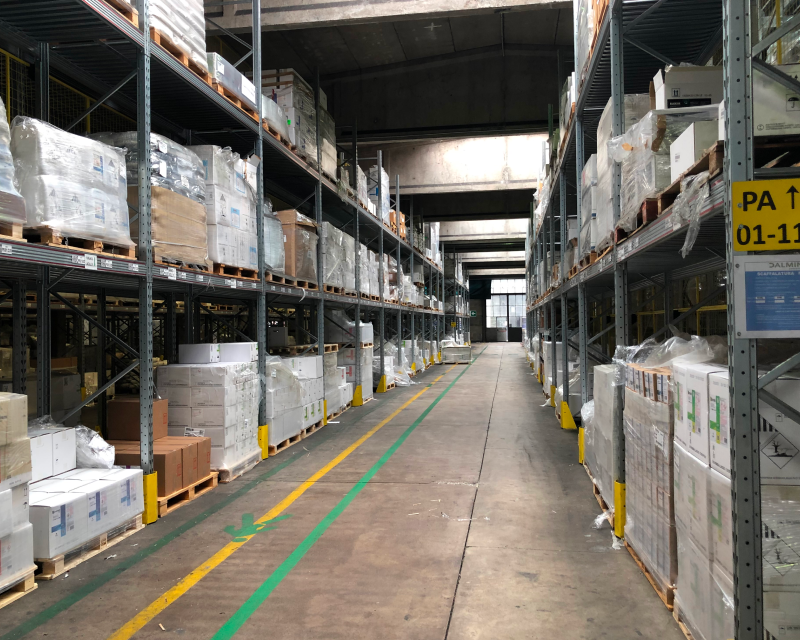
Our Logistics department ensures seamless supply chain management by leveraging an efficient bonded warehouse system. This allows us to safely manage inventory and guarantee reliable worldwide shipments to our global partners.